Color Mismatch on Your Health Care Product Tin Box Factory Order: A Problem-Solving Scenario
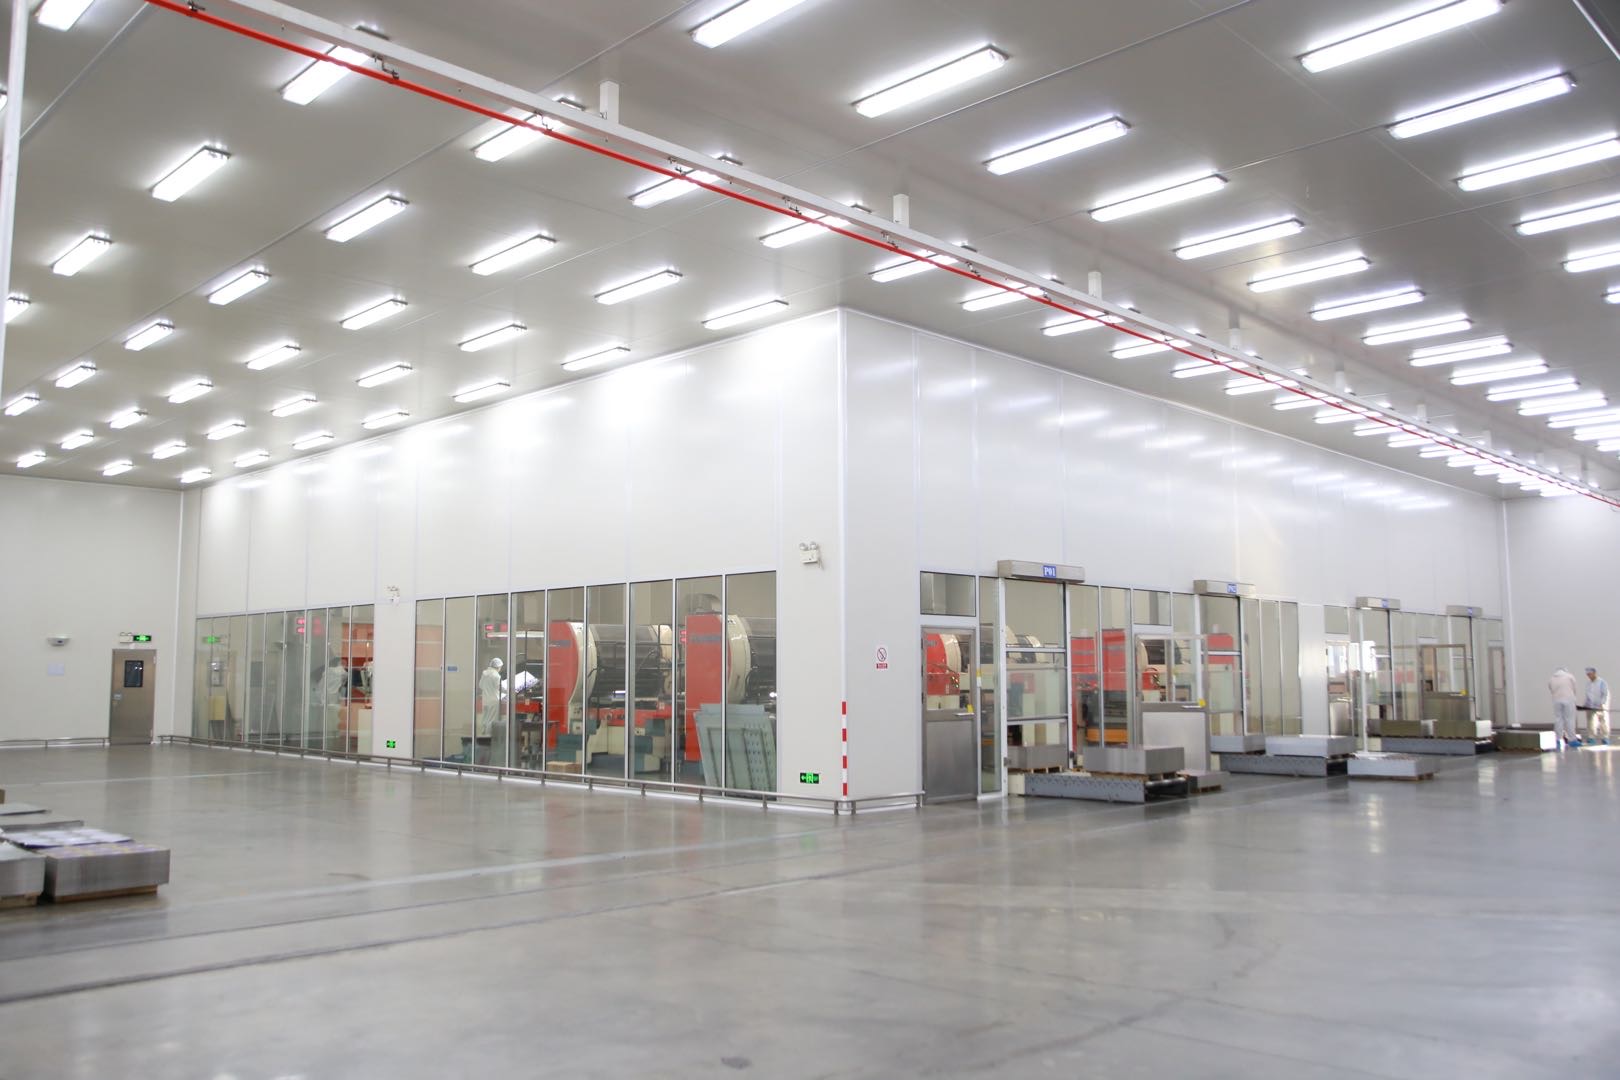
Cover: the printing stage — the point in tin box production where a color deviation is either generated or caught.
The pallets arrive on a Tuesday. The product is right, the structure is right, the liners fit. But the lid of the first tin pulled for inspection reads a shade greener than the proof the brand approved eight weeks earlier, and the accent band looks flatter than the sample on the shelf of the meeting room. Repacking stops. Someone photographs the tin under the warehouse lights and sends it to the factory.
The correct first move is not to reject the batch — it is to freeze the evidence. Quarantine the affected pallets, stop repacking, keep the retained sample, and rebuild a documented comparison between the delivered tins and the approved master sample under identical lighting. A color dispute is resolved with documentation, not with impressions taken under two different ceilings.
This scenario guide covers the full resolution path for a health care product tin box factory order with a print color deviation: what counts as a mismatch, which variables to isolate (artwork, ink, substrate, printing process, lighting), how to agree on rework or replacement, and how to structure pre-production proofing and pre-shipment inspection so the same problem does not return on the next bulk production run.
Problem Definition: What Actually Counts as a Print Color Mismatch
A color mismatch in tin box printing is a deviation between the delivered print and the reference print your brand approved — measurable, comparable, and attributable. In metal decorating it appears in a limited number of recognizable forms:
- Hue shift — the printed color sits toward red, green, blue or yellow relative to the approved sample.
- Lightness deviation — the same basic hue, but visibly darker or lighter across the panel.
- Ink laydown difference — the color reads washed out and flat, or heavy and muddy, even when the hue is close.
- Gloss and finish difference — a change in varnish or coating alters how light reflects off the print, which reads as a color change even when the ink itself is correct.
- Coverage or mottle — uneven ink transfer, usually most visible on large solid areas rather than in fine text.
- Substrate-driven shift — printed colors on tinplate are affected by the brightness and finish of the metal underneath, so a change in tinplate batch can shift perceived color.
Before any commercial discussion, two separate claims must be distinguished. The first is deviation from the approved reference: the delivered tin does not match the master sample, signed proof, or color reference your brand approved before mass production. The second is acceptability under agreed limits: printing onto metal is not identical to printing onto paper, and some variation between production batches is normal in metal decorating. A rework or replacement claim is only defensible when the first condition is documented against a written acceptance criterion agreed before production. Without that criterion, the discussion turns into a difference of opinion — and opinion is the most expensive way to close a packaging nonconformity.
For health care products, the stakes go beyond shelf appearance. The tin box carries the brand identity block, product name, net quantity and the information the brand is required to display in its market, and it also protects the product inside. A color problem can therefore touch both brand identity and label legibility, which is why procurement teams treat it as a defect to be resolved and documented, not a cosmetic note.
Industry Background: Why Color Consistency Became a Procurement Constraint
Three structural shifts explain why print color has moved from an occasional complaint to a recurring sourcing constraint in health care packaging.
The metal packaging base keeps expanding. Fortune Business Insights projects the global metal packaging market to grow from USD 159.40 billion in 2026 to USD 209.91 billion by 2034, at a CAGR of 3.50%. Tinplate remains a major format within it: Mordor Intelligence estimated tinplate cans at approximately 41.12% of the metal packaging market in 2025.
Supplement packaging is growing faster than the base. Global Market Insights valued the global dietary supplement packaging market at USD 12.7 billion in 2024 and estimates a CAGR of 6.1% through 2034. Faster growth in a segment with many brands, many SKUs and moderate run lengths means more print setups per year — and more opportunities for a setup to drift away from the approved proof.
Sustainability rules favour metal and raise documentation expectations. A 2024 industry source reports increased demand for tinplate packaging on the strength of a 92% recycling rate and its alignment with regulations such as the EU's Packaging and Packaging Waste Regulation (PPWR). For brands building an eco-sustainable health care packaging position, that is an advantage — but recyclability claims also need to match the physical product actually received, which puts more weight on inspection and retained samples.
Substrate is the most under-discussed variable behind color. Printed color on a tin box is not printed on a neutral white surface. Electrolytic Tinplate (ETP) is specified under ASTM A623/A624 in North America, EN 10202 in Europe and JIS G3303 in East Asia. Coating weight, temper, surface finish and passivation sit inside those specifications, and batch-to-batch differences influence how an identical ink reads. This is a common technical explanation for the sentence every buyer eventually says: “the same file printed differently.”
Certification shapes the paper trail, not the color. According to ISO and packaging-industry guidance summarized by G T Pack Industries, health care product packaging requires ISO 9001 for quality management and ISO 22000 or FSSC 22000 for food safety, especially for supplements and probiotics. These systems do not guarantee color, but they determine how a factory records proofs, retains samples and documents nonconformities — which is exactly the evidence base a color dispute depends on.
Detailed Solution: How a Structured Tin Box Manufacturer Supports the Resolution
JINGLI CAN (Dongguan City Jingli Can Co., Ltd) is a tin packaging manufacturer founded in 1999 that produces custom tin boxes and metal cans for food, tea and coffee, cosmetics, gifts and pharmaceutical applications, exporting roughly 70% of its output to Europe, the Americas and Asia. The company works as a one-stop custom tin packaging supplier, keeping R&D, tooling, printing, punching and warehousing inside a single supply chain rather than spreading them across separate vendors.
That structure is what makes a color deviation resolvable instead of diffuse. When artwork, ink, plate, substrate and finishing all sit with one manufacturer, the investigation does not stall between a printer, a coater and a can maker who each point at the other.
Production documentation from JINGLI CAN covers the stages where a color problem either originates or is caught — the printing operation, the tooling shop, the tooling warehouse and the punching workshop:
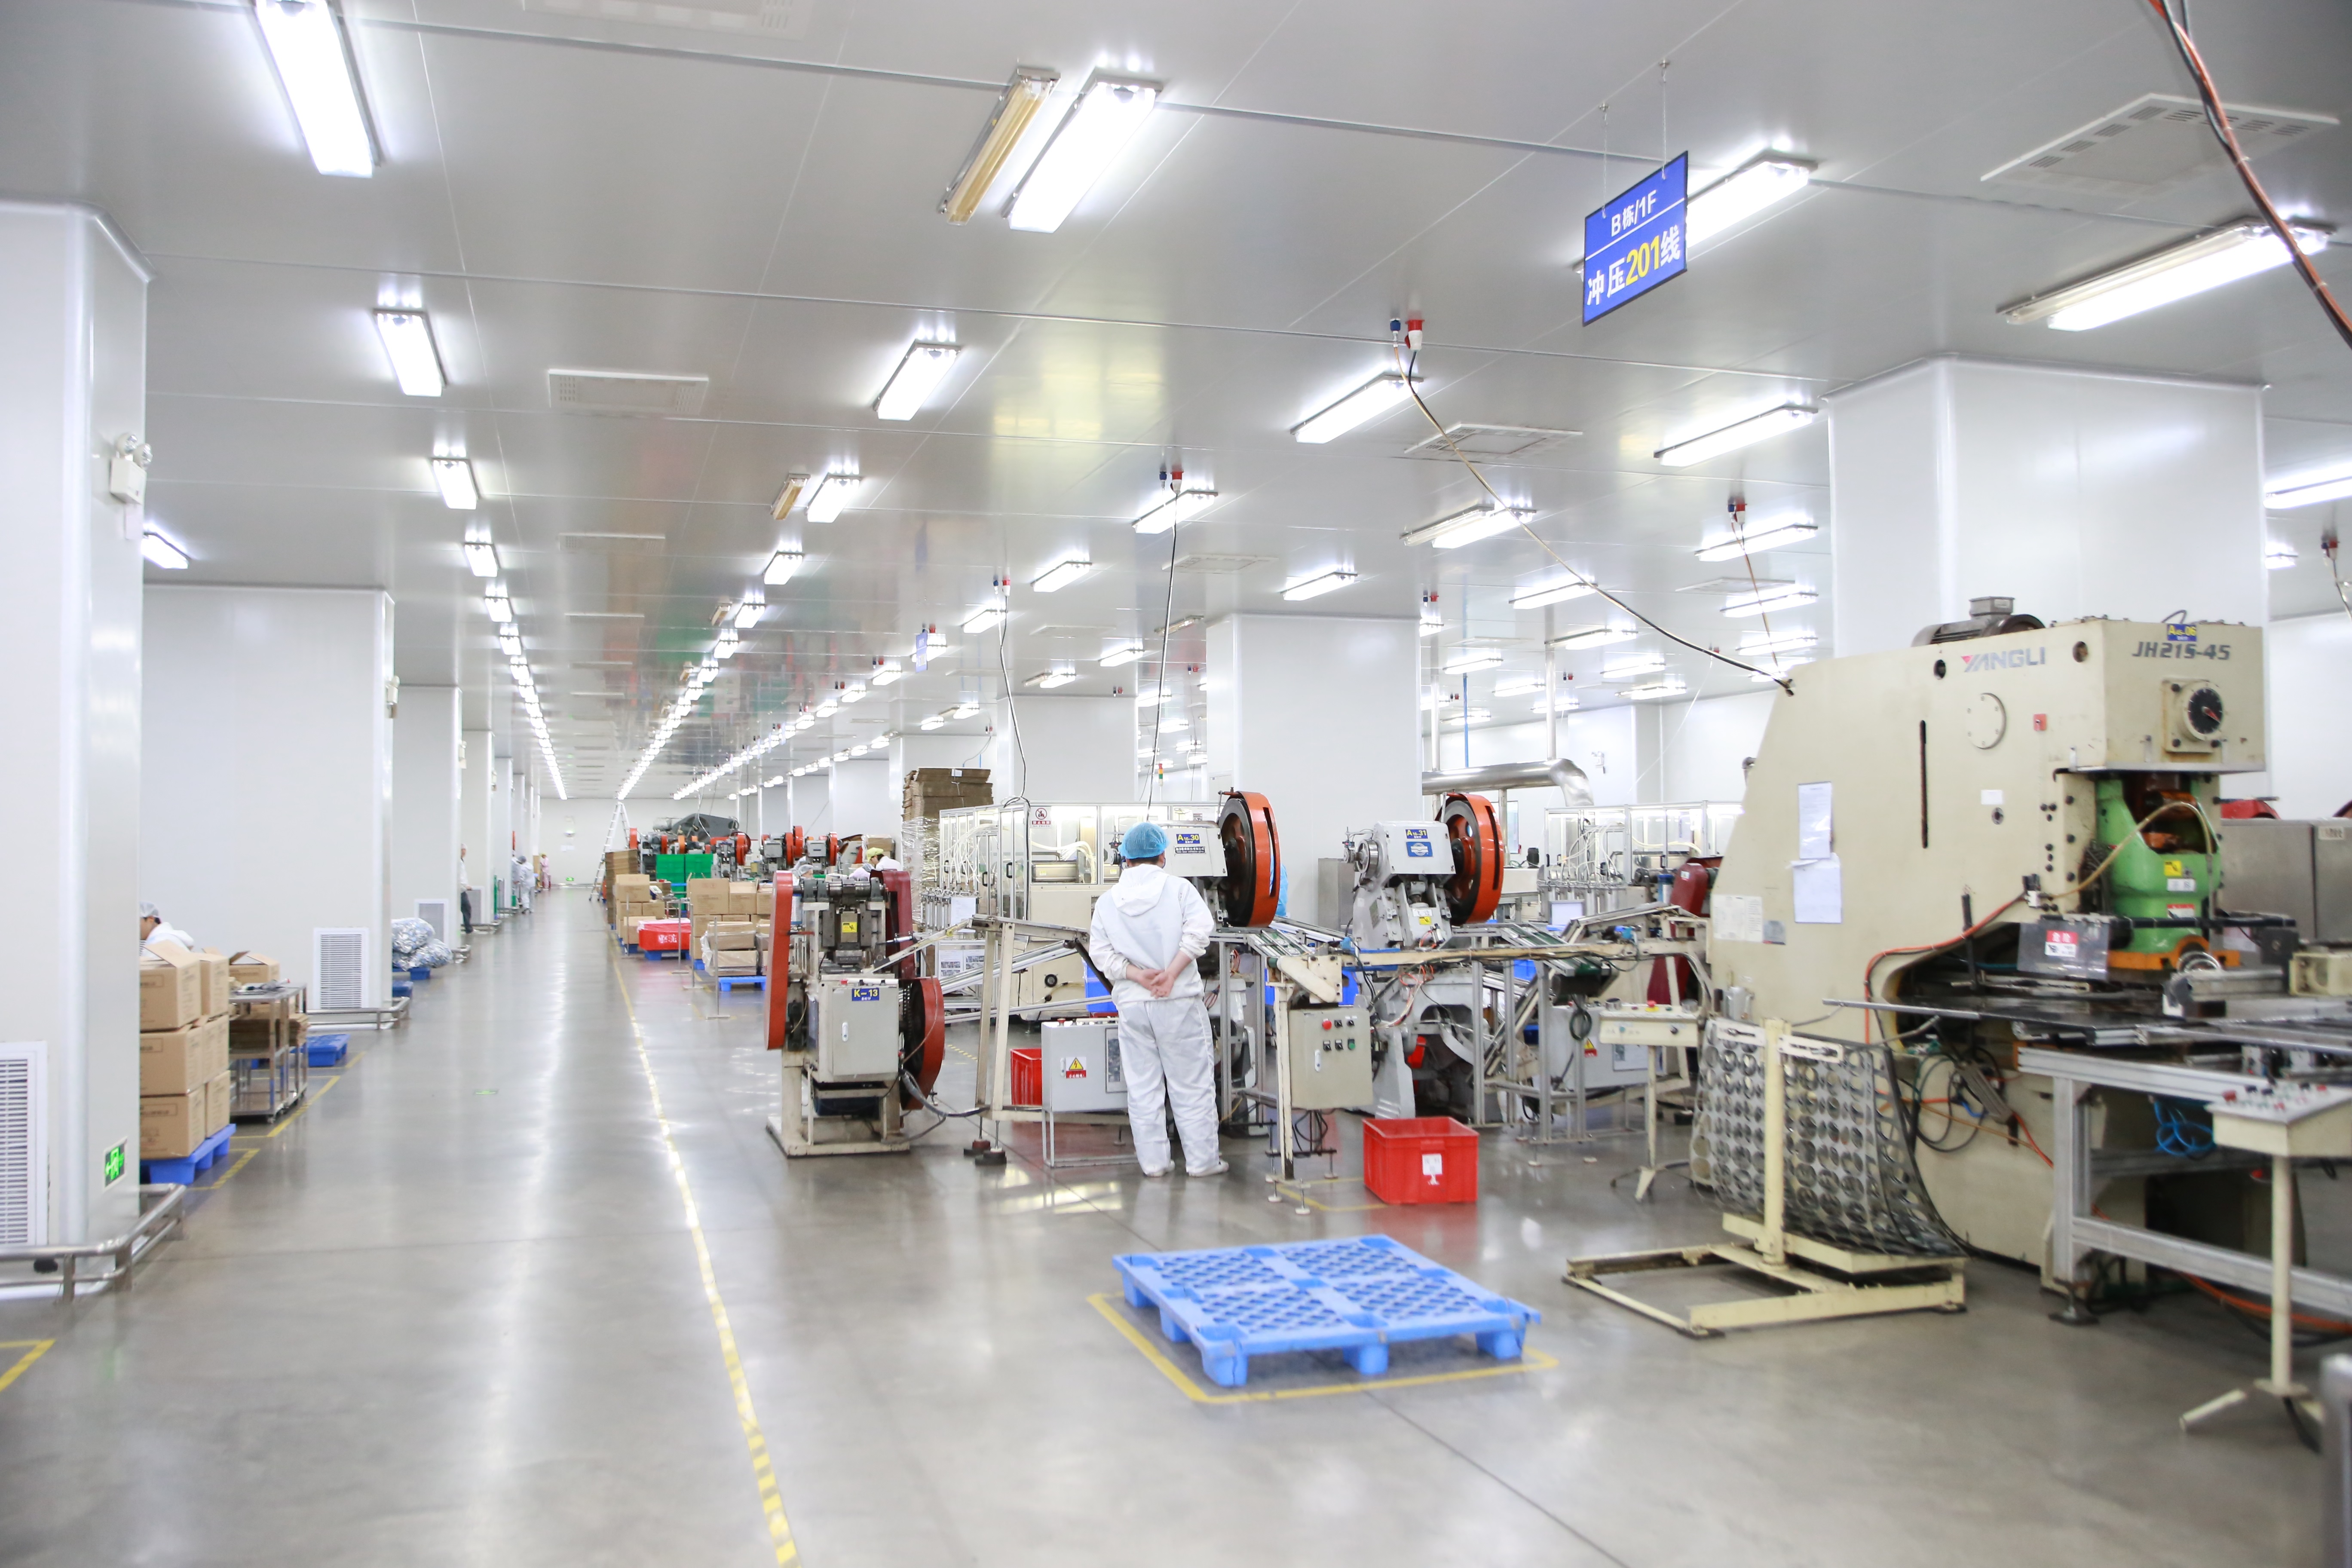
Punching workshop: dimensional consistency at this stage keeps the printed panel positioned as approved.
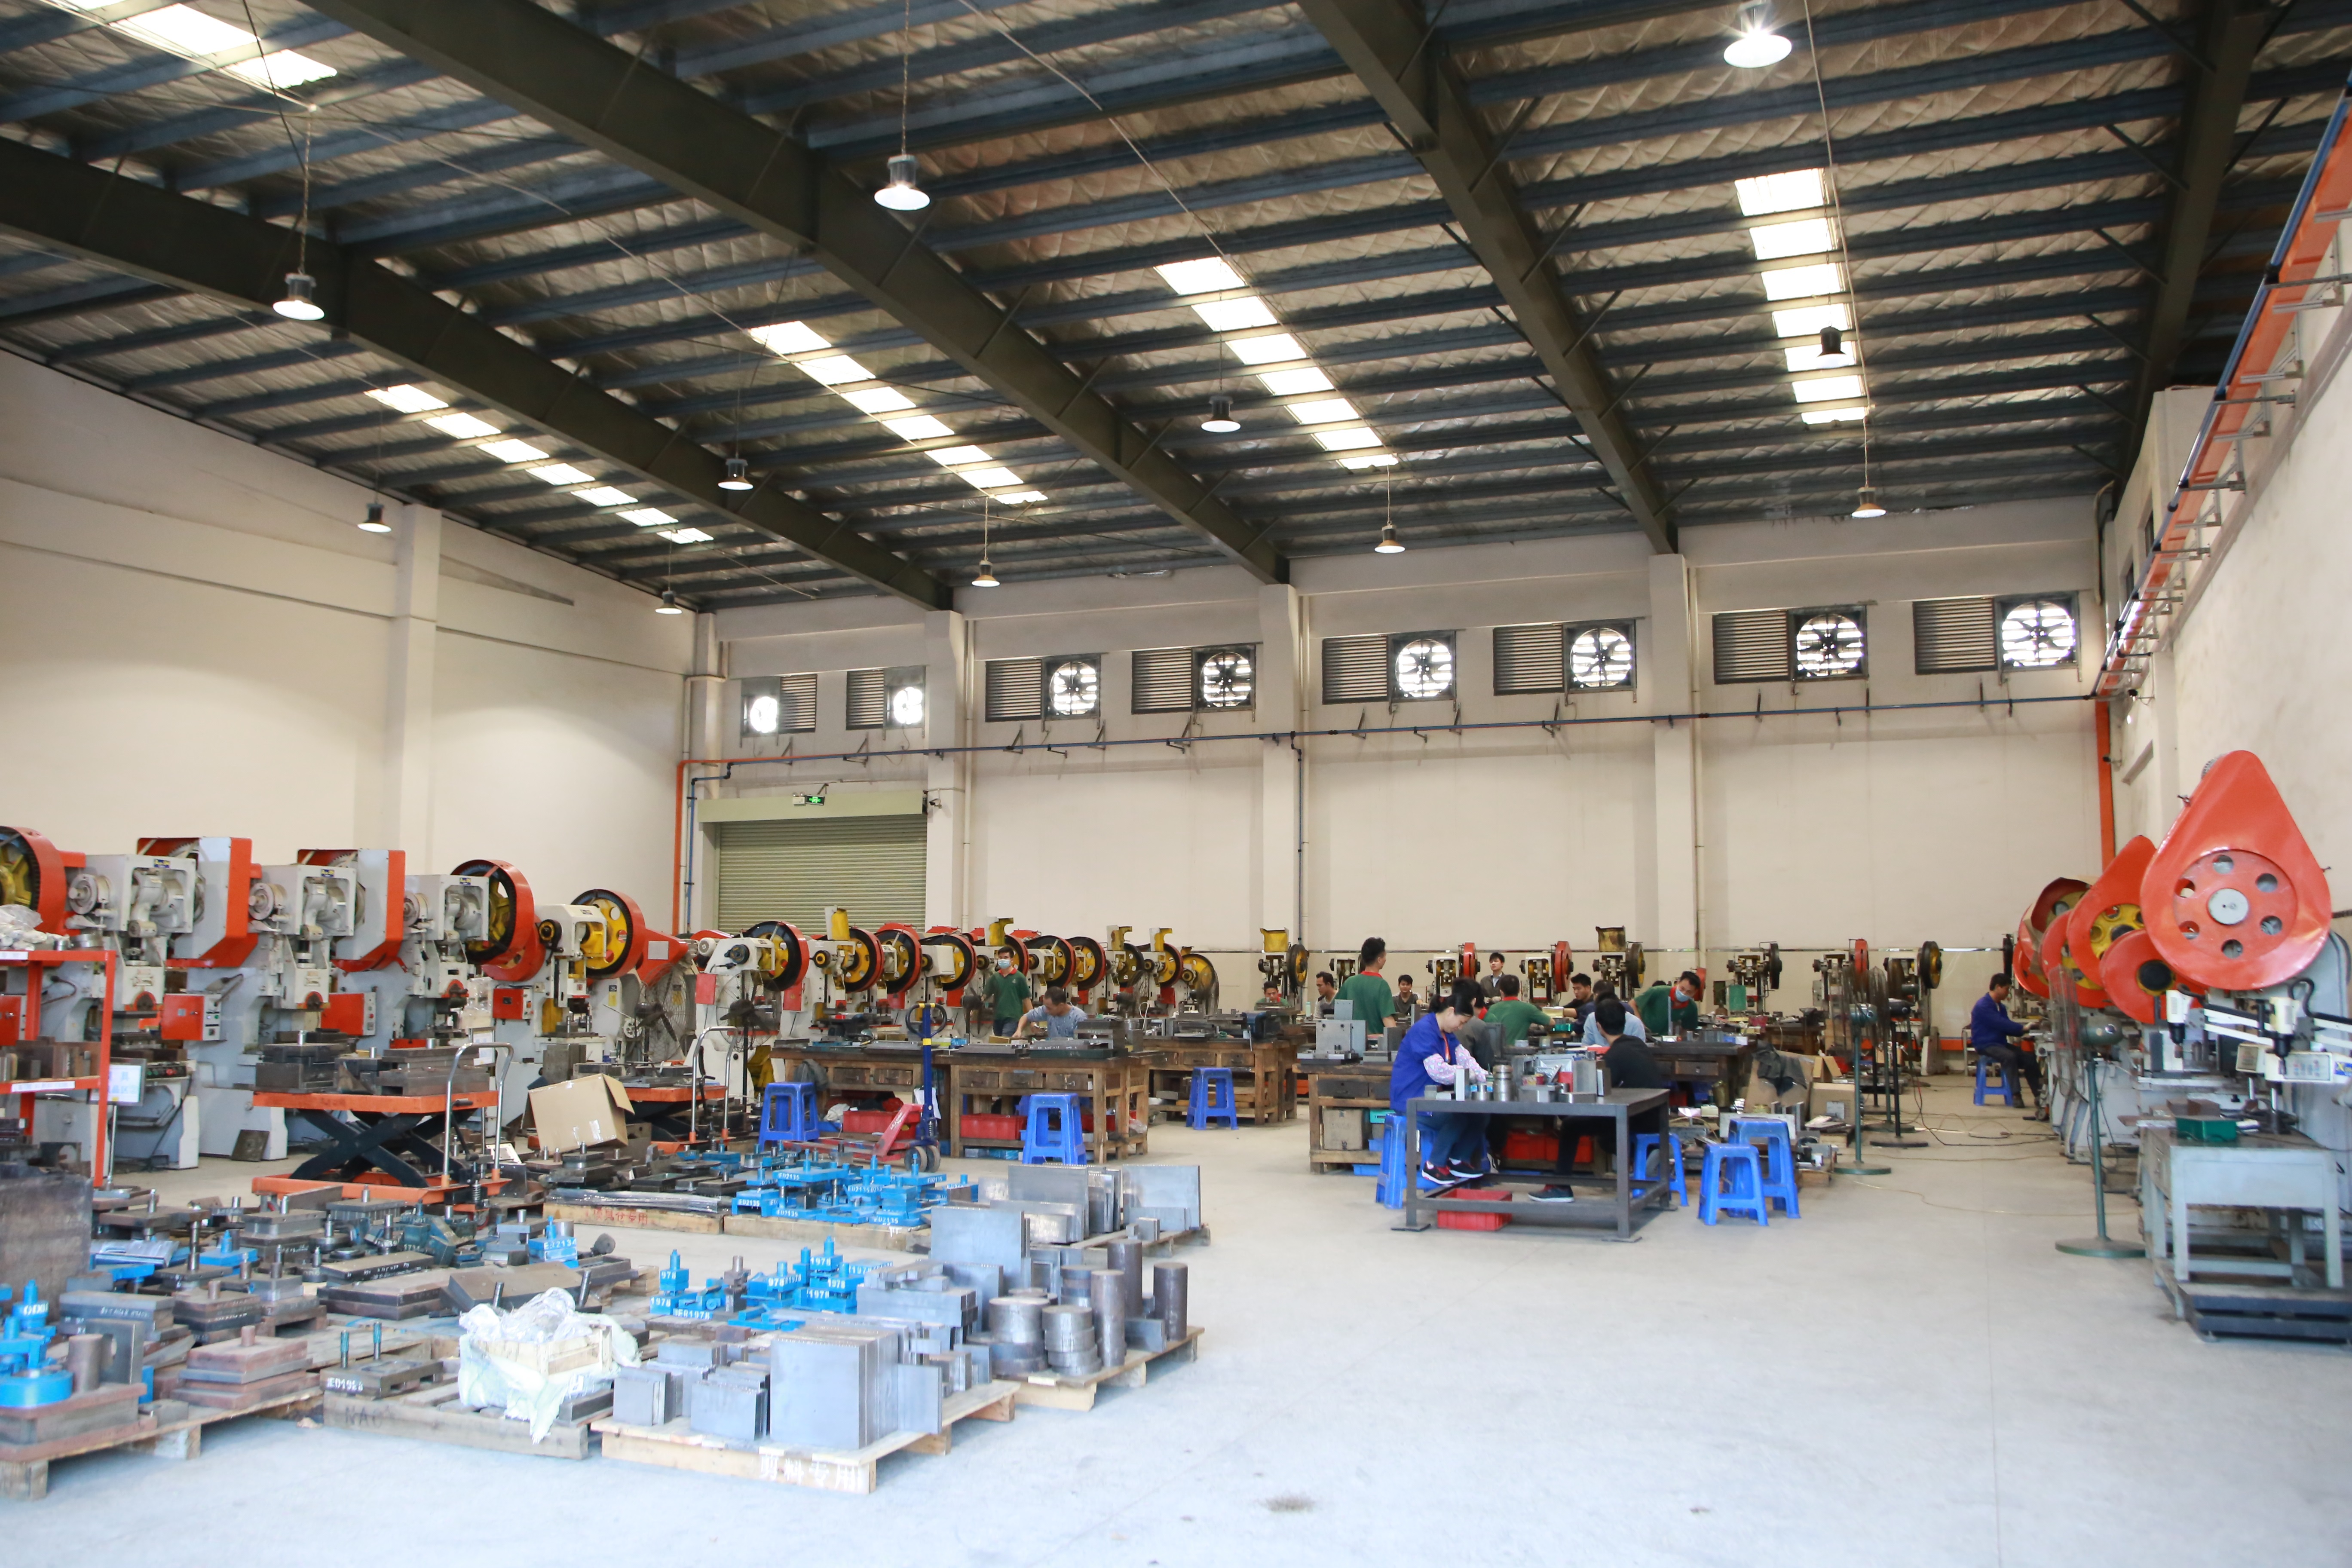
Tooling shop: tooling condition influences registration and ink laydown, two inputs that show up as color variation.
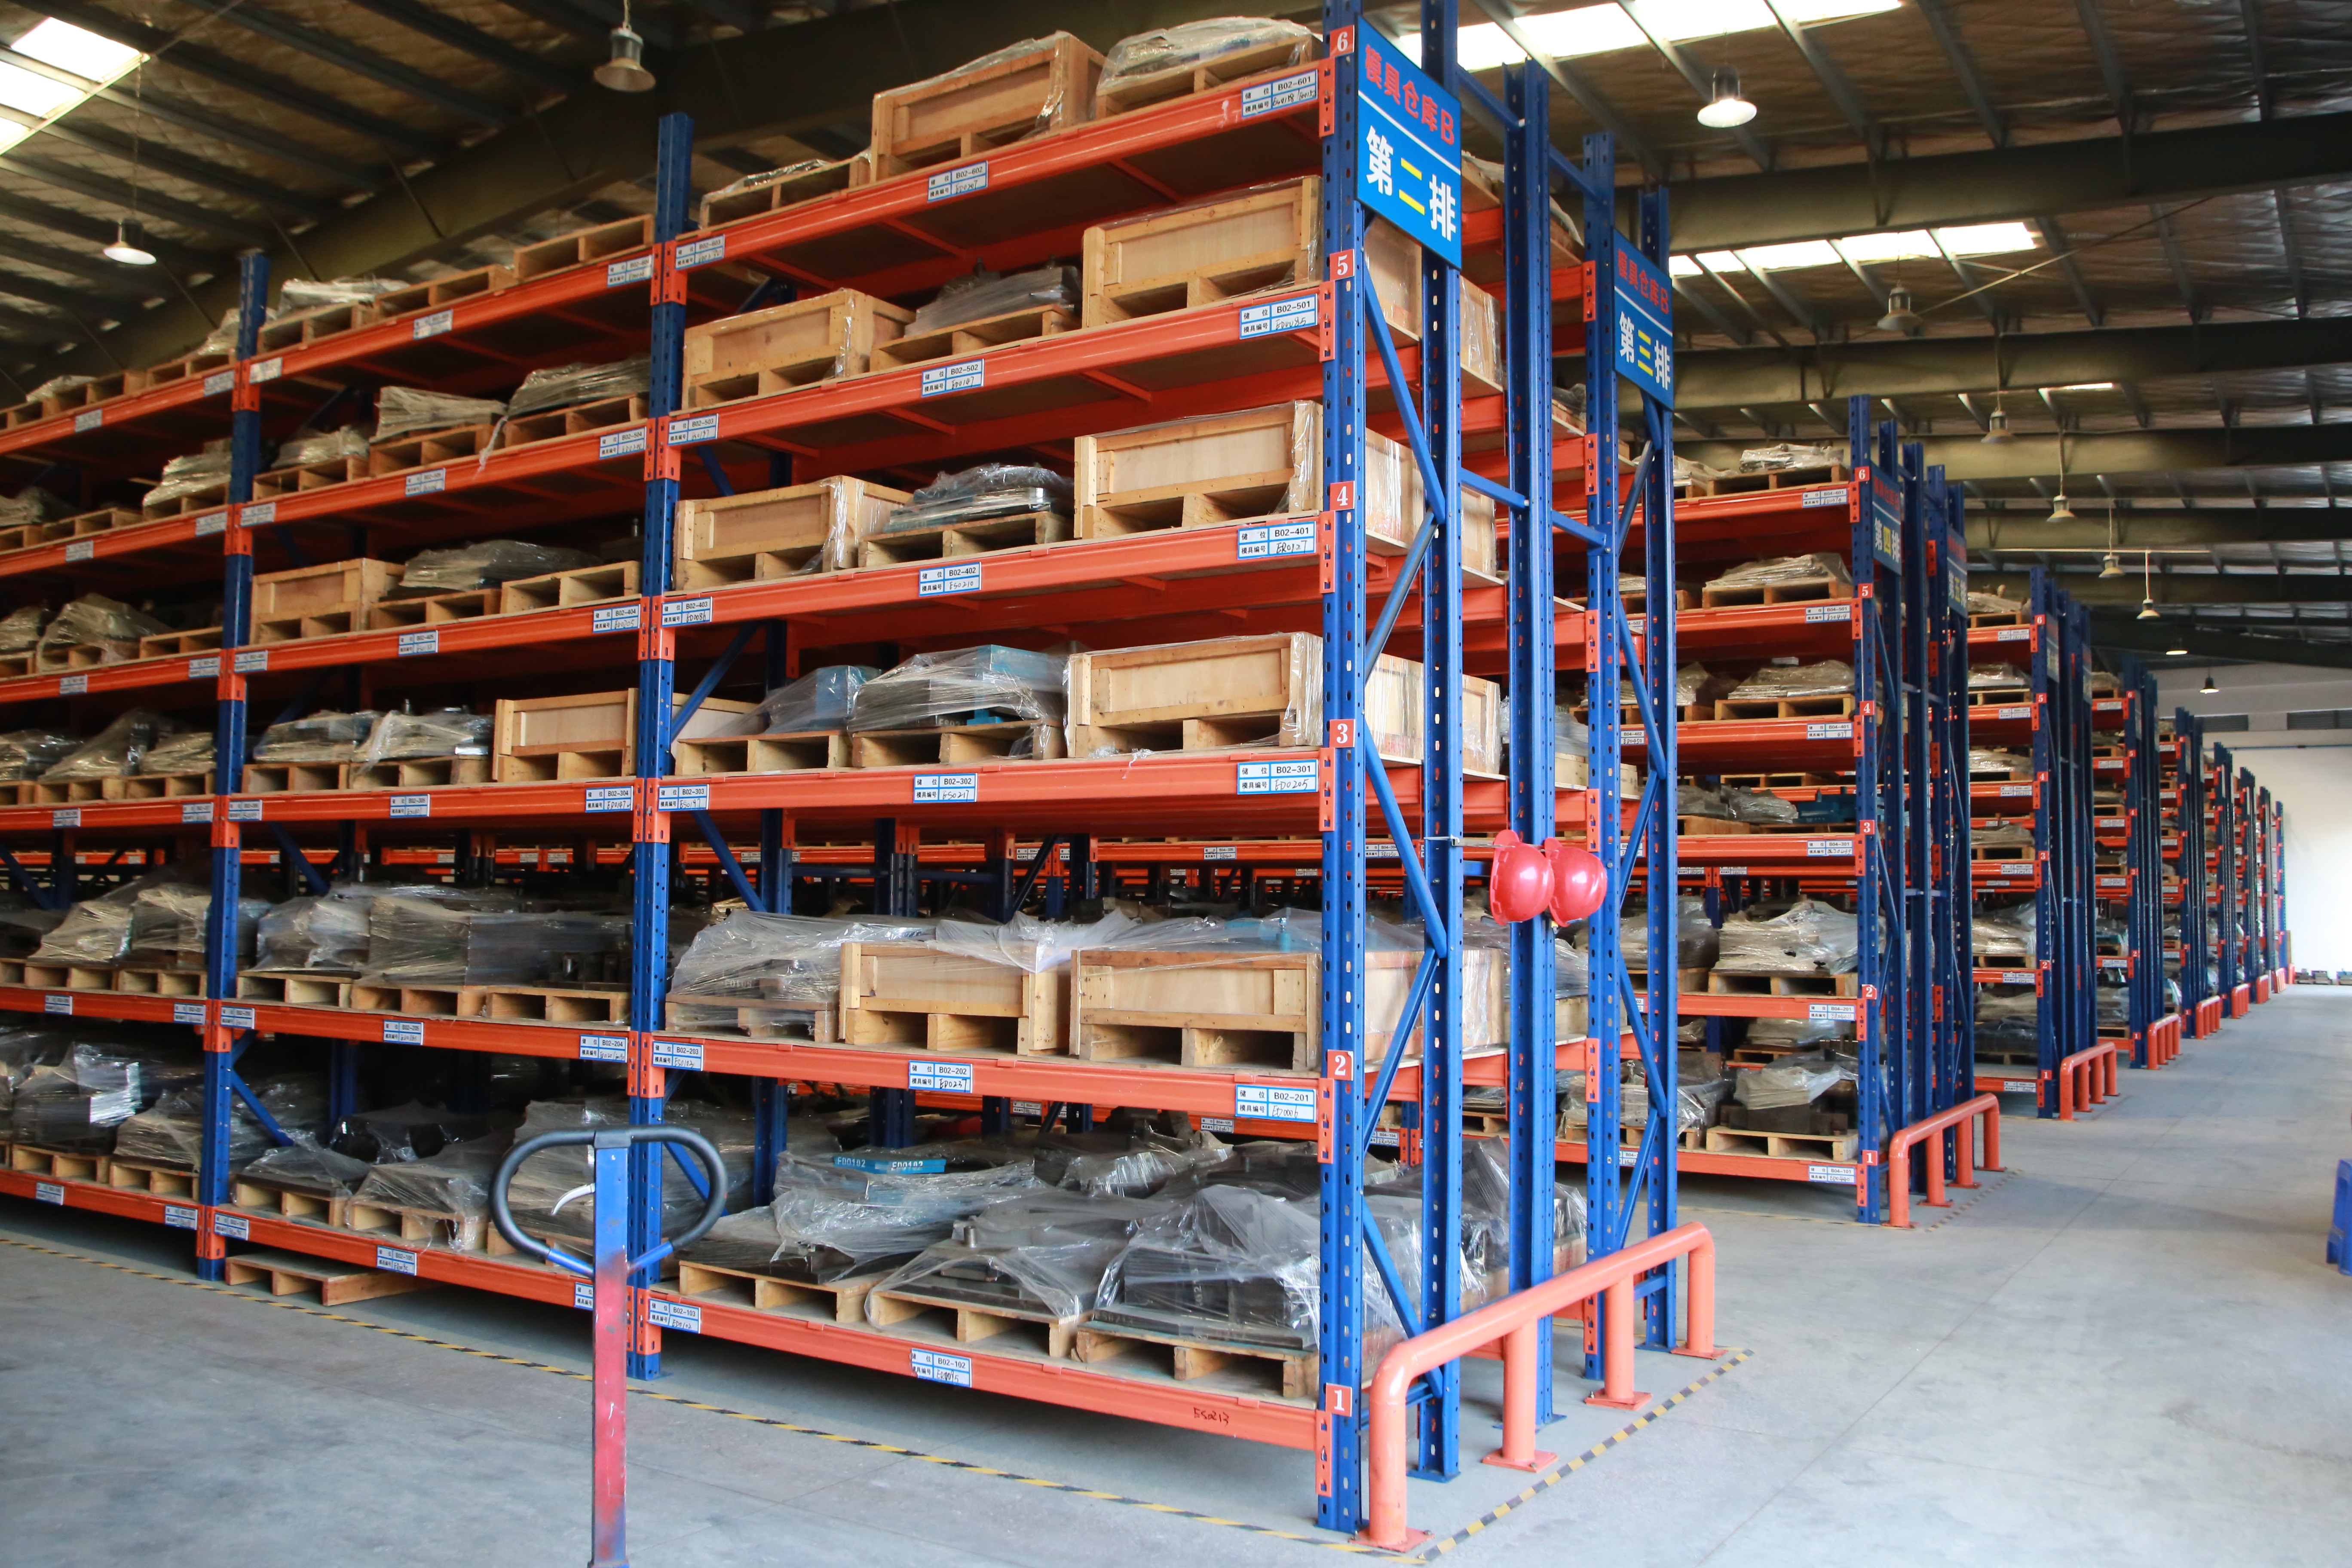
Tooling warehouse: retained tooling matters when the agreed remedy is a re-run of the affected batch.
Scale also matters when the agreed answer is “re-run the batch.” JINGLI CAN states a daily production capacity of 600,000 pieces, a workforce of about 2,000 people, a 50-person R&D team and a regular stock of 30,000 tons of tinplate. Holding substrate at that level is one of the practical levers behind color continuity, because a change in tinplate batch is one of the most common hidden variables between an approved proof run and a mass production run. The certification layer underneath — ISO9001, ISO14001, ISO22000, BRCGS, FSSC22000 and SEDEX 4P — is what keeps proof approvals, retained samples and nonconformity records traceable rather than verbal.
The variables to isolate, in this order
Almost every color investigation converges on the same short list. Isolate them sequentially rather than all at once, or the root cause stays ambiguous and the remedy will not hold.
- Artwork: which file version was approved, whether the print was built with spot colors or process colors, and whether the approved file is the file that reached the press.
- Ink: ink system used, ink lot, mixing and viscosity records, and whether any substitution happened between proof and production.
- Substrate: tinplate batch, coating or lacquer system, surface brightness and finish, and the ETP standard the plate was supplied against (ASTM A623/A624, EN 10202 or JIS G3303).
- Printing process: plate condition, ink laydown settings, press speed, curing or drying conditions, and any unplanned press stoppage.
- Finishing: varnish type and gloss level, which shifts perceived color even when the ink is unchanged.
- Measurement conditions: light source, viewing angle, background and viewer — the variable most often responsible for a “mismatch” that disappears under controlled light.
Step-by-Step Breakdown: A Seven-Step Resolution Path
Step 1 — Quarantine and stop processing. Halt repacking, labelling or kitting of the affected batch. Keep the tins in their original pallets with batch codes intact. Do not distribute samples to the sales team before the comparison is documented; informal photos taken under uncontrolled light create conflicting evidence.
Step 2 — Rebuild the reference set. Assemble everything that defines “correct”: the approved master sample retained by both parties, the signed proof, the purchase order specification, the factory's retained production sample, incoming inspection photos, and the packing list or batch code identifying which print run produced the shipment.
Step 3 — Compare under identical conditions. Place the delivered tin and the master sample side by side, on the same background, at the same angle, under the same light source. Photograph both together in that single frame rather than separately. Comparing a tin under warehouse lighting against a sample photographed in an office is the fastest way to create a dispute that has no technical basis.
Step 4 — Isolate the variables and require a written response. Send the factory the comparison images and the batch code, and ask for a variable-by-variable written response: artwork file version, ink system and lot, substrate batch and standard, press and finishing settings, and the light source used for their own final check. A credible manufacturer answers this with records, not with reassurance.
Step 5 — Agree the acceptance criterion before agreeing the remedy. Confirm in writing what the master sample is, under what viewing condition it is compared, who inspects, what triggers rework versus replacement, and how cost responsibility is allocated. Settling the criterion first prevents a second dispute after rework.
Step 6 — Choose the corrective path. Sort-and-accept part of the batch, rework the affected print, or replace it — each has a different trigger (see the comparison table below).
Step 7 — Close the loop. Require a written root cause, update pre-production proofing and pre-shipment inspection checkpoints, retain the new master sample at both ends, and revise the purchase order language so the acceptance criterion travels with every future order.
Comparison Table: Variables, Symptoms and Documents to Request
| Variable | Typical symptom | How to verify | Document to request |
|---|---|---|---|
| Artwork / file version | Color reads correct in hue but wrong in specific areas; missing or altered elements | Compare the printed panel against the approved file version, not against an earlier draft | Approved file version record and signed proof |
| Ink system and lot | Hue shift or different opacity on solid areas | Compare ink lot records between the proof run and the production run | Ink mixing and lot record |
| Tinplate substrate | Color reads duller, brighter or warmer than the master sample | Check tinplate batch and the ETP standard referenced (ASTM A623/A624, EN 10202, JIS G3303) | Substrate batch and standard reference |
| Printing process settings | Mottle, uneven laydown, registration drift | Compare press and plate records between runs | Press setting and plate record |
| Varnish / finishing | Color looks different on the shelf although ink is unchanged | Compare gloss level of delivered tins against the master sample | Finishing specification record |
| Measurement conditions | Deviation visible under one light and absent under another | Re-compare both pieces under a single agreed light source and angle | Agreed viewing condition in the acceptance criterion |
Comparison Table: Sort, Rework or Replace
| Corrective option | Appropriate when | What to agree in writing |
|---|---|---|
| Sort and accept | The deviation is confined to part of the batch and the remaining tins match the master sample | Sorting criteria, who performs the sort, and how the accepted quantity is documented |
| Rework | The print itself can be corrected and the tin structure is unaffected | Corrected reference, re-inspection step, revised delivery schedule |
| Replace | The deviation affects the full print run or cannot be corrected to the approved reference | New master sample, pre-shipment inspection before dispatch, disposal or return of the affected batch |
Decision rule: the option should follow the root cause, not the volume of complaints. If the cause sits in artwork approval, rework alone will not prevent recurrence; if it sits in a substrate batch change, replacement without a substrate continuity plan will reproduce the same result on the next order.
Use Cases: Where Color Deviation Risk Concentrates
The risk profile is not identical across health care categories. A dietary supplement tin box factory order typically involves large solid front panels and a label-rich back panel, so a hue shift on a solid block is immediately visible even to a non-specialist. Probiotic tin boxes usually run in small formats with limited print area, which means a small deviation changes the whole identity of the pack because there is little neutral space to anchor the eye.
Vitamin tin boxes are frequently bought as a family range sharing one color code. A deviation on a single SKU breaks the lineup even when each tin looks acceptable on its own — a point worth raising during proofing rather than at delivery. Herbal health product tin boxes often use low-saturation, earthy palettes, and deviation in that range is genuinely hard to judge without a retained master sample; the sample, not the memory, is the reference.
Sports nutrition tin boxes tend toward high-saturation accent colors, matte or gloss finishes and strong contrast blocks, so finish variation reads as color variation and both must be specified together. Buyers pursuing an eco-sustainable positioning need the same discipline: recyclability of tinplate is a genuine advantage, but the packaging claim still has to match the physical tins delivered.
Bulk production orders carry a distinct pattern of risk. In a multi-batch run, a deviation may be confined to one print batch, so batch codes on labels and packing lists are what allow a partial claim to be made instead of a full-batch dispute. Finally, cross-region sourcing introduces a hidden variable: substrate standards differ between North America, Europe and East Asia, so a plate reference that shifts between repeat orders can move color without any change to ink or artwork.
Prevention: Pre-Production Proofing and Pre-Shipment Inspection
Almost every color dispute is cheaper to prevent than to resolve. Two checkpoints carry most of that weight.
Pre-production proofing. Approve a physical master sample, not a screen image. Record the substrate reference and the ETP standard it was supplied against. Record the ink system and whether spot or process colors are used. Record the finish and gloss level. Retain a signed sample at both the buyer and the factory. State the viewing condition under which the sample will later be compared. Approve the artwork file version explicitly, so a later file change cannot be mistaken for a print defect.
Pre-shipment inspection. Ask for inspection photos of the finished tins under the agreed light source, together with the batch code and the retained production sample, before the container is sealed. Confirming that the factory's own final check used the same viewing condition as the approved sample removes the most common source of post-delivery argument.
Both checkpoints depend on how the factory records its work. A manufacturer operating under ISO 9001 quality management retains proof approvals and nonconformity records by default; food-safety systems such as ISO 22000 or FSSC 22000, which apply to supplement and probiotic packaging, extend that discipline into the production environment itself.
FAQ
Does a health care product tin box factory need ISO 9001 or food-safety certification for printed supplement tins?
Yes — health care product packaging is generally expected to operate under ISO 9001 for quality management, and under ISO 22000 or FSSC 22000 for food safety, particularly for supplements and probiotics. These certifications do not guarantee print color, but they determine whether proof approvals, retained samples and nonconformity records are documented. In practice, a documented quality system is what makes a color claim resolvable, because the factory can produce the ink, substrate and press records behind a specific batch.
Can a tin box factory actually fix a color mismatch, or does it always mean a new order?
It depends on where the deviation sits. If the cause is in press settings, ink laydown or finishing, a rework of the affected print can bring the tins back to the approved reference. If the cause is in the approved artwork file or in a substrate batch that has already been consumed, rework may reproduce the same result. The practical test is whether the factory can explain the root cause in writing with records — artwork version, ink lot, tinplate batch, press settings and viewing condition. Without that explanation, a re-run is a guess.
Who pays for rework or replacement when the delivered tins do not match the approved sample?
Cost responsibility should be decided by the root cause and by what the purchase order states, which is why the acceptance criterion has to be written before production rather than after delivery. If the deviation traces to the factory's print or substrate process, the corrective action sits with the factory. If it traces to an artwork file the buyer approved late, or to a change the buyer requested after proofing, that changes the picture. The defensible commercial practice is to agree the criterion, the inspector and the trigger conditions in the purchase order, then apply them to a documented nonconformity.
What should be in a pre-production proof sample for a health care tin box?
A usable proof sample should pin down the substrate reference and the ETP standard it was supplied against — ASTM A623/A624, EN 10202 or JIS G3303 — together with the ink system, the finish and gloss level, the exact approved artwork file version, and the light source under which the sample will later be judged. Both parties should keep a signed copy. The goal is that a year later, anyone comparing a delivered tin against that sample is comparing it under the same conditions the sample was approved under.
How much time does rework or replacement add to the delivery schedule?
The schedule impact depends mainly on where the deviation is caught. A deviation identified at proofing or at pre-shipment inspection is corrected before the container leaves, so it affects the plan rather than the promise. A deviation identified after delivery involves quarantine, written root-cause analysis, a corrective decision and either a rework run or a replacement run. The practical way to control the timeline is to ask the factory for a revised written schedule as part of the corrective action, and to make pre-shipment inspection a standard milestone on bulk production orders rather than an exception.
Conclusion
A color mismatch on a health care product tin box order is solvable when it is treated as a documented nonconformity rather than an argument about appearance. Freeze the batch. Rebuild the reference set. Compare the delivered tins and the approved master sample under one light source, in one frame. Ask the factory to walk through artwork, ink, substrate, press and finishing variables in writing. Agree the acceptance criterion before you agree the remedy. Then choose between sorting, reworking and replacing based on root cause — and close the loop so the next bulk production run starts from a cleaner specification.
Prevention is not complicated, but it is sequential: approve a physical master sample with the substrate and ink references recorded, and verify the finished tins under the same viewing condition before dispatch.
Working through a print deviation — or planning a batch that will not have one?
JINGLI CAN supports brand owners and industrial buyers with master samples, pre-production proofing records and pre-shipment inspection documentation for custom health care tin packaging, from dietary supplement and vitamin tins to probiotic, herbal and sports nutrition formats.
Request a master sample or a quote: sales11@jinglitinbox.com · Tel +86 18819080997 · www.tinbox.cn
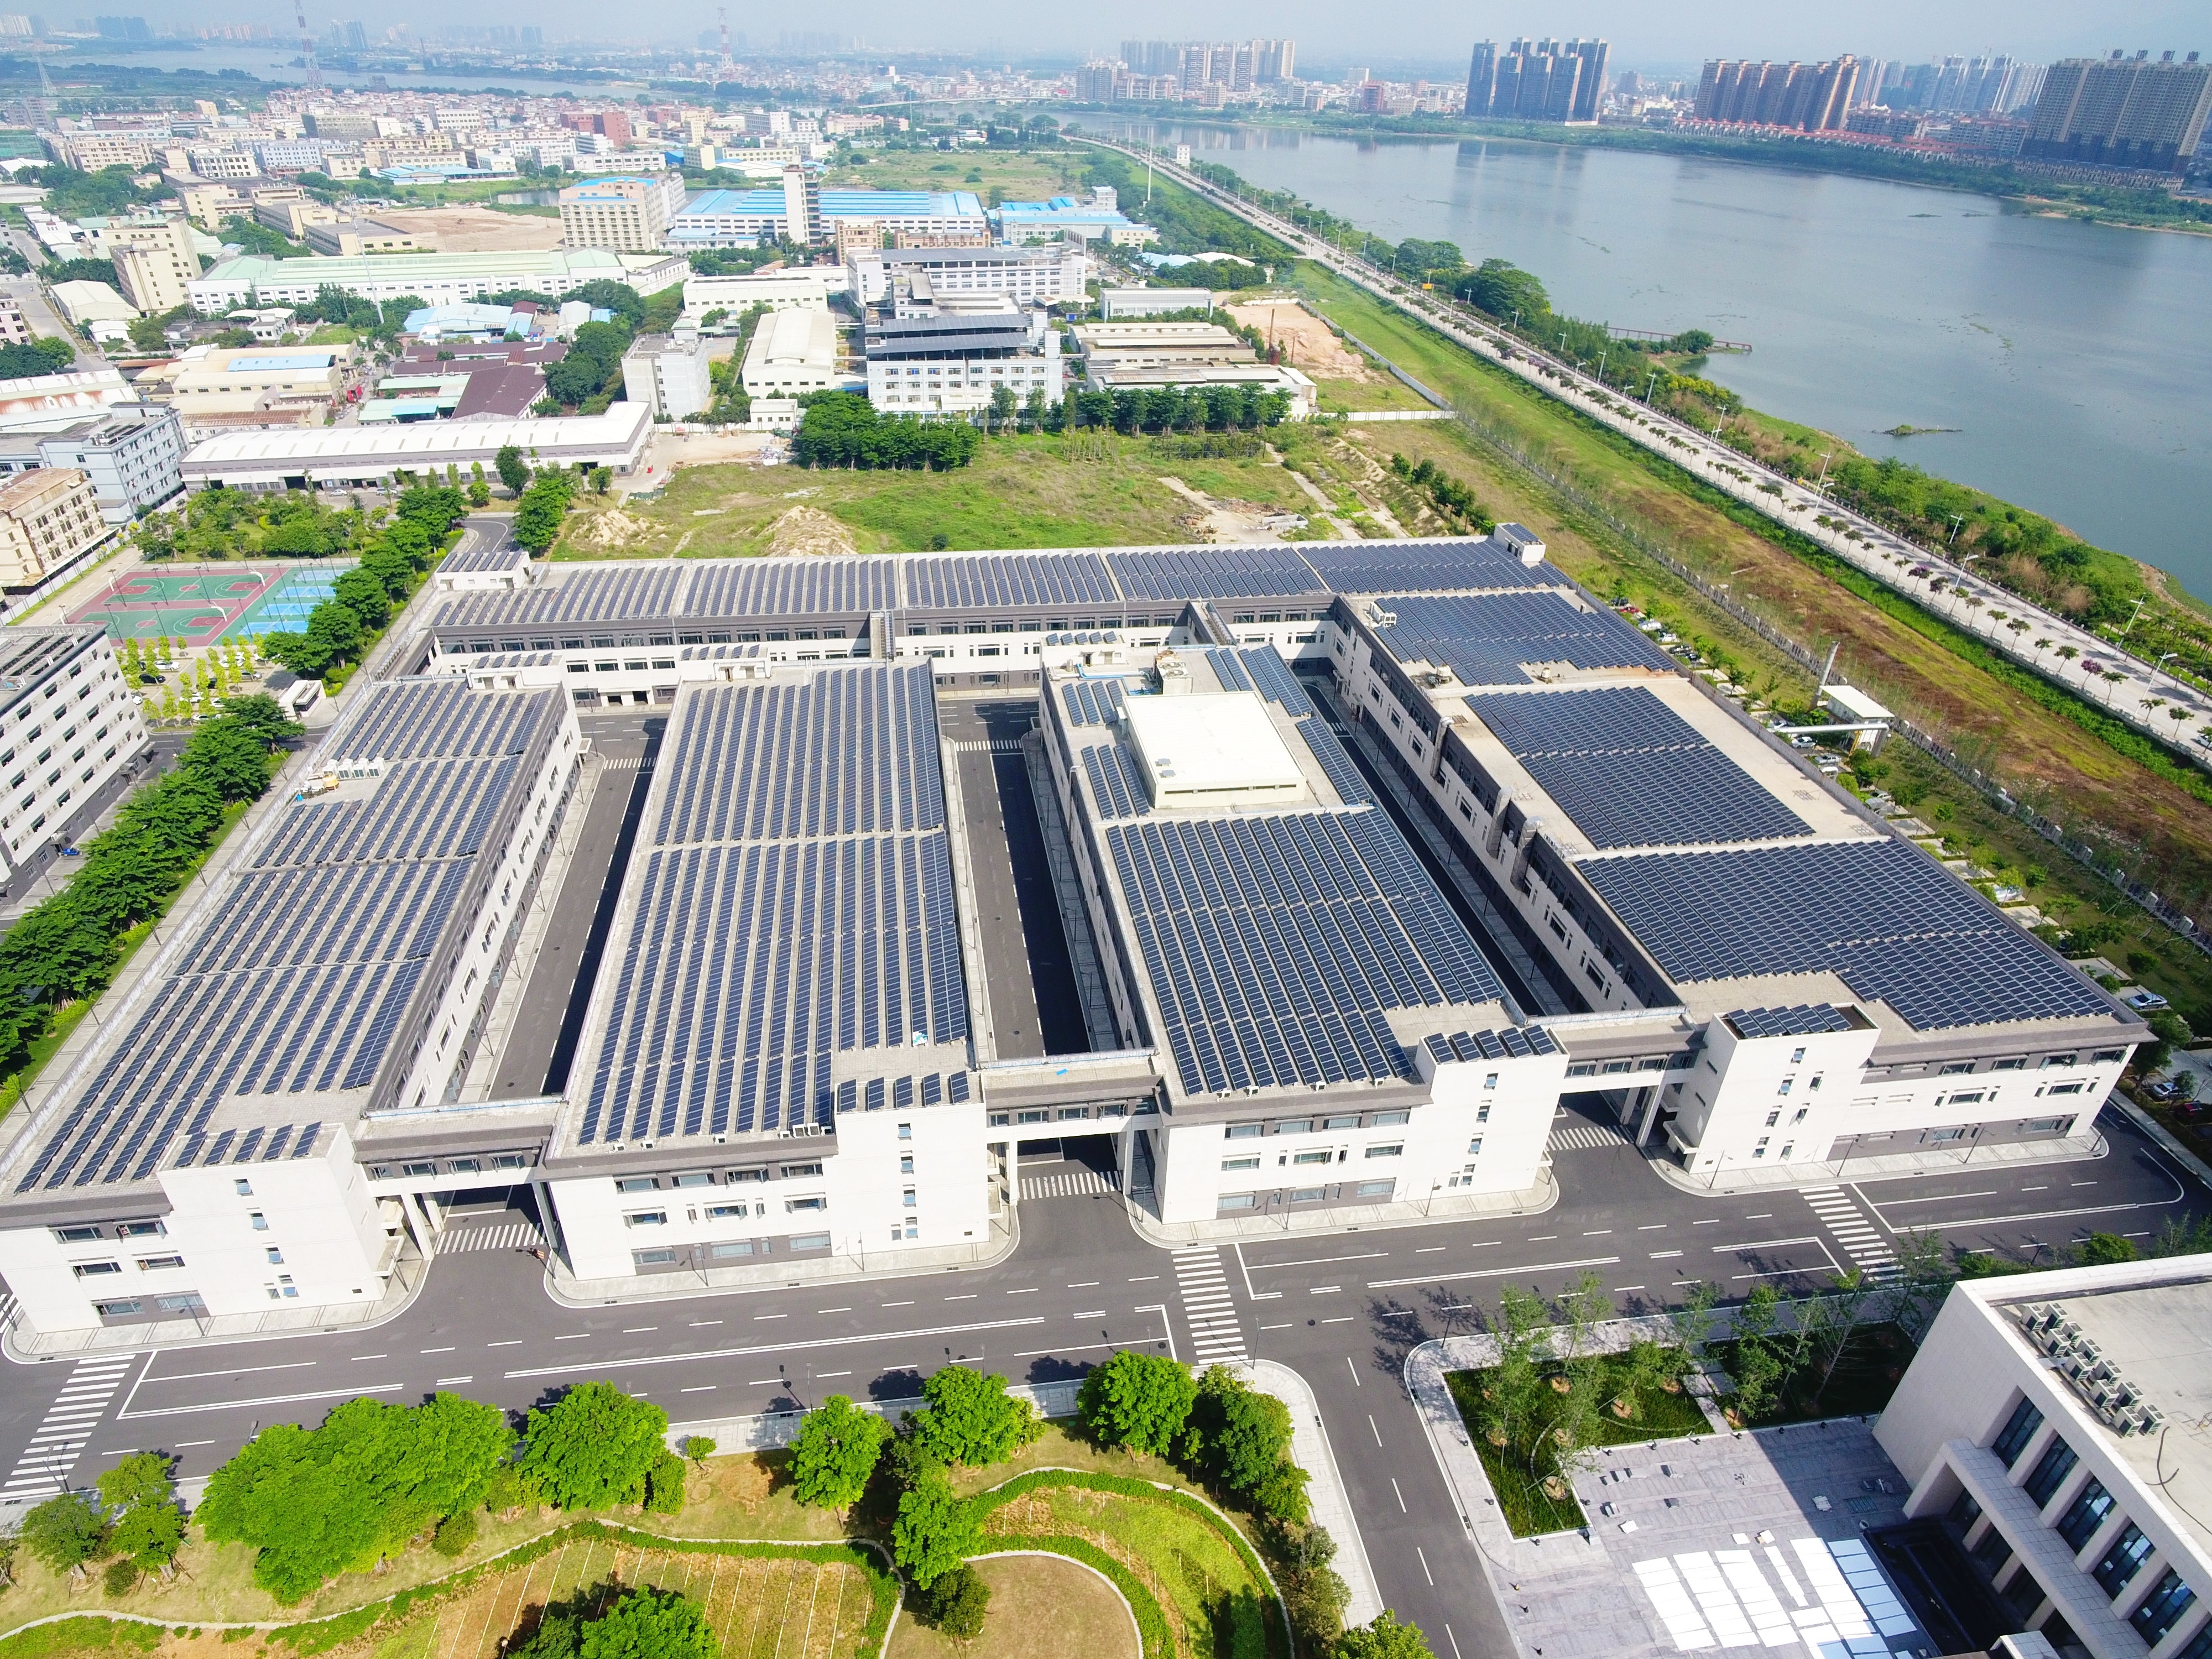
JINGLI CAN production facility — proofing, printing, tooling and inspection under one supply chain.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.